
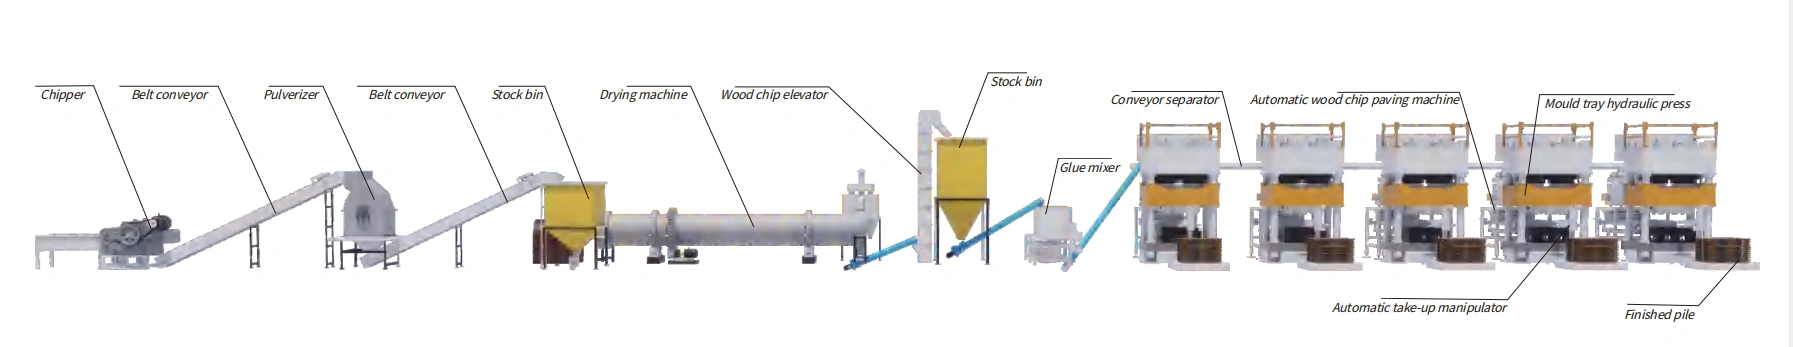
The Scenario: Pellet Plants Pay for Every Oversize Particle in the Feed
A pellet mill only performs as well as the particles it receives. When biomass feedstock arrives as a mix of coarse chunks, splinters, and fine dust, the press struggles to compress a consistent bed. The ring die runs hotter, the rollers slip on oversized pieces, and every ton that leaves the conditioner carries less mechanical strength than it should. For plants targeting ENplus A1 certification, where pellet mechanical durability must hold at ≥98%, uneven feed is a direct threat to the grade.
This is why the front end of a biomass pellet production line matters more than most operators assume. The Wood Crushing Machine sitting at the raw material entrance is not a simple size-reduction step; it is the control point that decides whether the press consistently receives flowable, uniform material—or a stream of variable particles that punish the die, the drive, and the final durability score.
The Old-Solution Problem: Chippers and Shredders Do Not Deliver Uniform Feed
Many plants still prepare feedstock with equipment designed for other jobs. A wood chipper produces flat flakes sized for chipping contracts, not for a pellet die. A wood shredder reduces volume, but its output remains coarse and irregular—exactly the particle distribution that increases ring die wear and raises specific energy consumption per ton.
Manual splitting with saws or axes, where it still survives in smaller operations, makes the problem worse: batch sizes vary, particle geometry is never repeatable, and labor cost per ton is high. Plants that buy ready-made sawdust avoid the crushing step but inherit another problem—they pay for a material over which they have no particle size control, and any oversize fraction in the delivered lot lands directly in the press.
The common thread is the same: none of these approaches regulate output particle size at the front end, so the pellet mill is constantly absorbing inconsistency that shows up as durability losses and avoidable energy bills.
Why the PULVZ Wood Crushing Machine Fits: Particle Size Is a Design Feature, Not an Accident
The PULVZ Wood Crushing Machine treats particle size control as a primary function rather than a by-product of crushing. Its high-hardness screen, mounted below the crushing chamber, is the sizing gate: material circulates inside the chamber until it passes the mesh, and only particles that fit the opening are discharged. Because the screen is replaceable, the plant can dial the output to the exact band the pellet mill wants—typically uniform particles of ≤5mm—and lock it there.
Uniform ≤5mm particles feed the press evenly, improve pellet formation rate, and raise mechanical durability. The same consistency also protects the ring die: fewer oversized and undersized particles means less abrasion, lower specific energy consumption, and longer intervals between die changes. For pellet plants, the crushing machine therefore pays for itself in die life and kWh per ton, before counting the durability improvement in the certified product.
Structure and Parameters That Back the Claim
The machine’s construction is built for continuous industrial duty. Thickened manganese steel hammer plates handle abrasive feedstock and resist wear; a one-piece manganese steel liner keeps the chamber geometry accurate over time; dynamic balancing keeps the rotor stable at high speed; and the high-hardness screen resists deformation, so the sizing gate keeps its opening day after day.
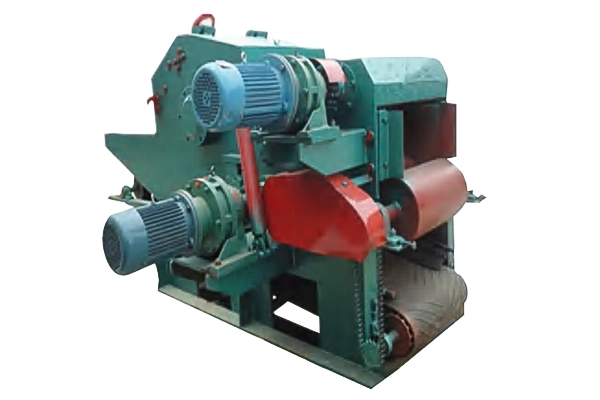
F-Series capacity and power across the range
The F-series covers plants from compact lines to high-throughput operations. The F-800 (780 mm screen, 45 kW) produces 1–2 t/h; the F-1000 (980 mm screen, 55 kW) delivers 2–3 t/h; the F-1200 (1180 mm screen, 75 kW, 2,000 rpm) reaches 3–5 t/h; and the F-1500 (1480 mm screen, 110 kW, 2,600 rpm) scales to 5–8 t/h. Inlet openings grow from 680×380 mm to 1350×450 mm, matching larger feed blocks on bigger lines.
Supporting details matter in daily operation. A magnetic separator removes tramp metal before crushing, protecting the rotor and keeping metal out of the finished feedstock. A cyclone separator handles dust collection and material–air separation at discharge, and the hydraulic open-cover system lifts the chamber top for fast hammer and screen maintenance—shorter downtime on the line.
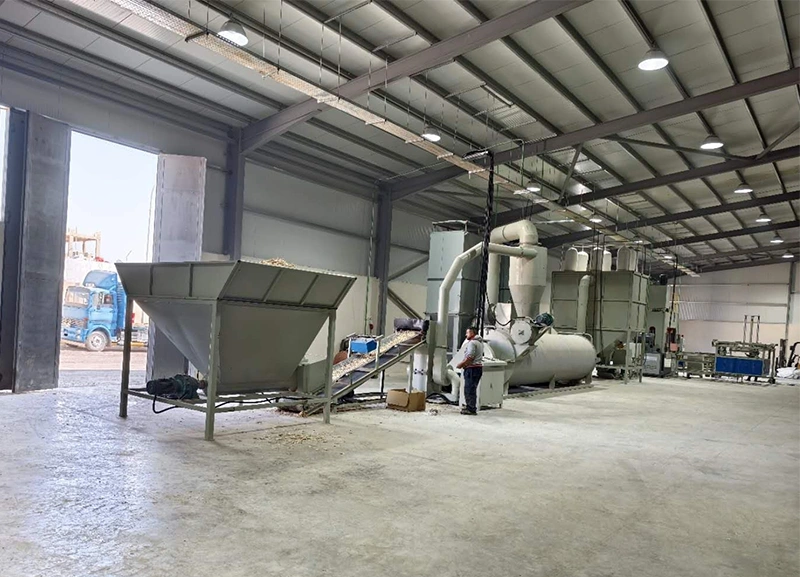
The Final Result: Consistent Feed, Certified Durability, Lower Ton Cost
With a Wood Crushing Machine controlling the front end, the pellet plant removes the largest variable from the press. Feedstock arrives as uniform ≤5mm particles with good flowability, the press forms pellets with a higher success rate, and mechanical durability holds where ENplus A1 demands ≥98%. Ring die wear drops because oversize particles no longer grind their way through the die holes, and specific energy consumption per ton falls with smoother pressing.
For plants expanding capacity or tightening quality targets, the fix is upstream. Replacing an uncontrolled crushing step with a screen-regulated Wood Crushing Machine turns the pellet mill’s most common hidden cost—unstable feedstock—into a measured, repeatable input.