Capex Discipline for New Wood-Based Plants
The Buyer Profile: New or Expanding Pellet, Pallet, and Biomass Plants
For a greenfield pellet plant or a molded pallet line that is still pre-revenue or just past break-even, picking the wrong industrial wood chipper is rarely a question of technology. It is a question of capex timing. The same physical machine can either lock up cash the operation cannot spare, or it can be sized to the current throughput and scaled upward only when the books justify the next step.
Why a European Turnkey Line Often Locks Up Capital Before It Earnns Back
The default comparison for any serious buyer is the European drum chipper line, names like Andritz or Bruks. These are excellent machines for thirty to sixty ton per hour operations and they come bundled with engineered chip handling, screens, and downstream integration that smaller plants do not need. The problem is not the engineering. The problem is the purchase profile. Quotes are typically non-public, sized for much larger throughput than a four to twelve ton per hour plant can absorb, and packed with auxiliary equipment that the buyer does not yet have the labor or the floor space to operate. The result is straightforward. The mid-size plant either stretches its cash to buy capacity it cannot run, or it stays on the small chipper it already owns and watches its growth ceiling get hit two quarters earlier than projected. In both cases the capex is misallocated, and the only question is how long it takes to admit it.
Three Drum Chipper Tiers that Match Output to Capex, in Stages
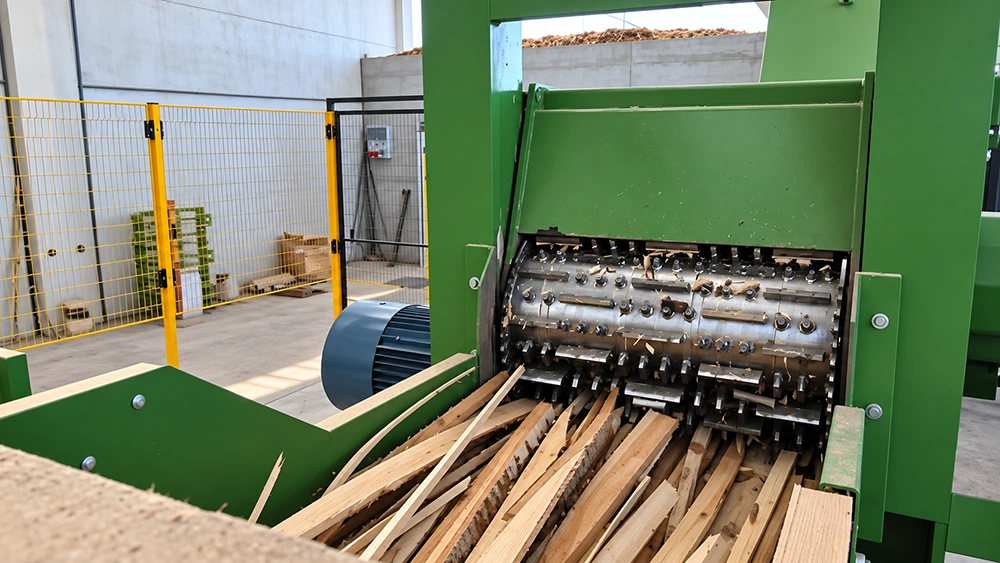
The EMP Shred drum wood chipper range is structured around three power and capacity steps so the buyer can match the machine to the current revenue curve rather than to a hypothetical peak. The X-215 ships at 45 kilowatts with a four to five ton per hour rating. The X-216 ships at 55 kilowatts with a six to eight ton per hour rating, which is the BX216 class output that most mid-size pellet and pallet plants actually need on day one. The X-218 ships at 110 kilowatts with an eight to twelve ton per hour rating for plants that have already proven the upstream feedstock and are ready to push the line. Each unit uses a hydraulic feed system with adjustable feed rollers, alloy steel fly knives on a rotating drum, and a sizing screen that holds the output to a thirty to thirty-five millimeter chip. The chip is uniform because the drum geometry and the screen work together, which is what lets the downstream hammer mill or refiner run at a stable load instead of choking on occasional oversize pieces. The same supplier can deliver just the chipper for a single-machine phase one, or the chipper plus hammer mill plus dryer for a full molded pallet line when the buyer is ready. That modularity is what lets a plant start with one chipper, prove the feedstock economics, and add the next stage of equipment only when the first stage is paid down.
What a Properly Sized Industrial Wood Chipper Buys You Back
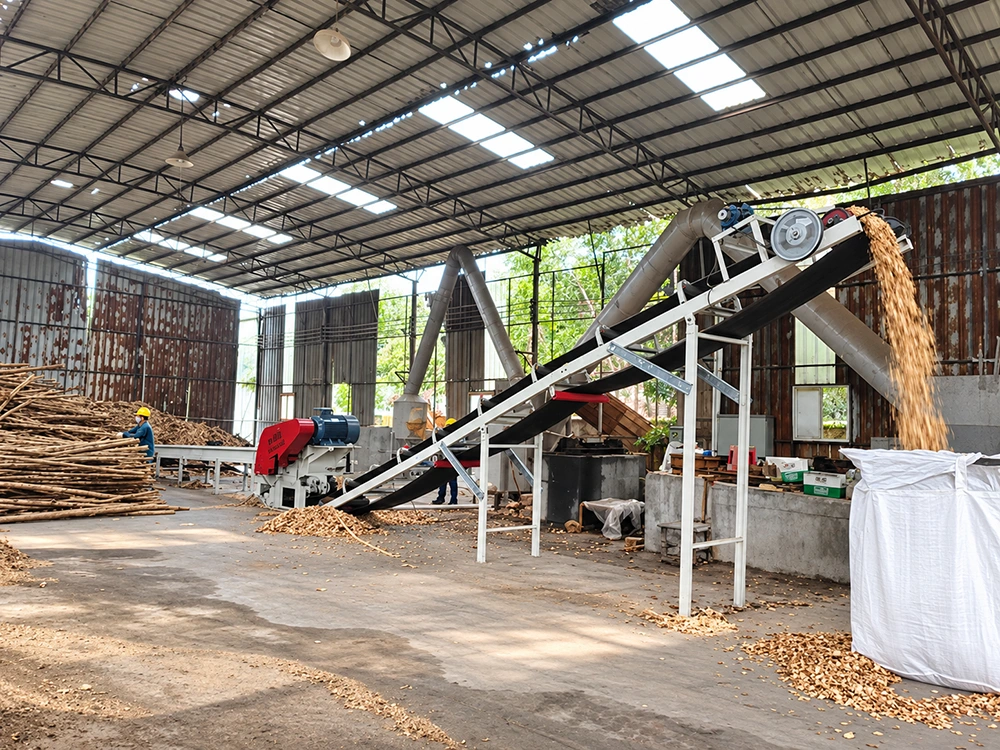
A drum chipper that is correctly sized to the current operation does three things to the operating account. First, it replaces the purchased chip or outsourced sawdust line item with internal production, which is the single largest variable cost swing available to a pellet or pallet plant. Second, the uniform thirty to thirty-five millimeter chip output lowers the kilowatt hour per ton that the hammer mill stage draws downstream, because the refiner is not chewing through random slab offcuts. Third, the hydraulic continuous feeding removes the manual feed labor from the upstream end of the line, which on a single shift operation is one operator per shift rather than two. When the chipper is sized correctly to the revenue curve and not to the wish list, the payback window is short enough that the second machine, the X-218 step or the additional downstream stage, can be funded from the first machine cash flow rather than from the line of credit. That is the capex discipline a new or expanding plant actually needs from its industrial wood chipper purchase.
- Title and intro both contain industrial wood chipper
- Body sections count equals four with no HTML markup
- Both image alts contain industrial wood chipper
- Contact CTA href is /contact/


