Proposal-stage technical solution for project evaluation and configuration review. Final equipment selection, layout, utilities, certifications, operating parameters, and commercial terms require confirmation during technical discussions.
AutoML Molded Pallet Production Line | Technical Proposal
This proposal-stage technical concept outlines a modular production system for converting wood fiber, bamboo powder, straw, or similar plant-based materials into standardized molded pallets. The process integrates material preparation, drying, adhesive dosing and mixing, weighing, mold filling, hot pressing, demolding, and pallet stacking. Configuration can be adapted to site conditions, material availability, labor costs, utility capacity, production targets, and the intended pallet market.
Discuss your molded pallet production requirements with EMP: https://presswoodpallet.com/contact/
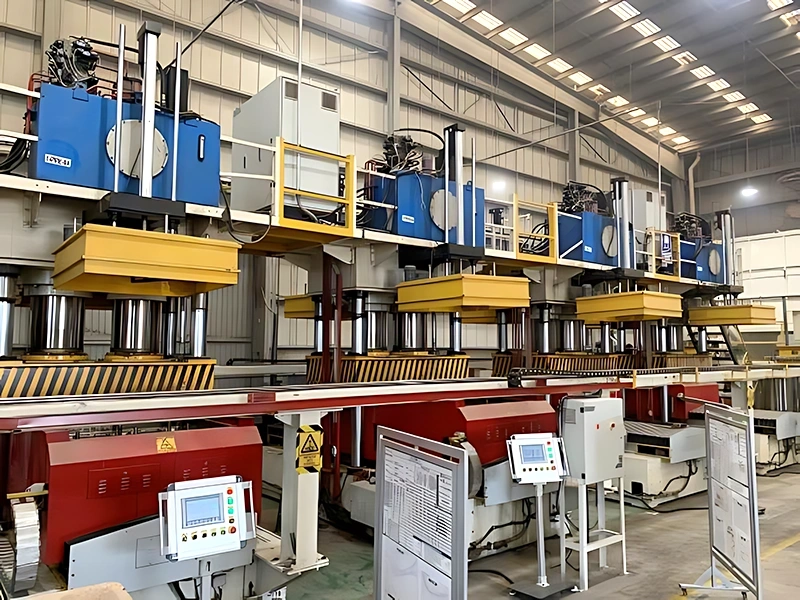
Plan for wood fiber or other plant-based material with a typical length of 5–30 mm, thickness of 2–5 mm, and mold-entry moisture content of approximately 6–10%. Material screening and iron removal should be considered when recycled pallet or wood waste is used.
Define pallet dimensions, mold cavities, shift pattern, operating hours, and target output. A reference automated configuration may be planned around approximately 1,200–1,600 pallets per 24 hours, subject to mold design, press count, cycle time, material handling, and utilization.
Confirm whether pallets are intended for domestic indoor circulation, heavy loads, humid conditions, food or pharmaceutical logistics, or export use. Adhesive type and dosage should be validated through trials; typical starting ranges are approximately 8–10% for MDI and 10–12% for UF or PF, subject to material and performance testing.
Key production and site-planning challenges
A molded pallet line must maintain consistent raw-material dimensions, moisture content, adhesive distribution, forming density, temperature, pressure, and cycle time. The project must also balance automation depth against available capital, local labor economics, maintenance capability, and expected production utilization. Dust-generating preparation equipment should be separated from adhesive, hydraulic, electrical, and forming areas to protect controls and improve operating safety. The intended pallet application also affects adhesive selection: MDI supports high strength, moisture resistance, and low-formaldehyde applications but has higher cost and greater mold-sticking risk; UF may suit lower-demand dry indoor applications; PF can be considered where heat and moisture resistance are required.
Project Requirements
| Input | Proposal-stage evidence |
|---|---|
| Raw-material preparation | Plan for wood fiber or other plant-based material with a typical length of 5–30 mm, thickness of 2–5 mm, and mold-entry moisture content of approximately 6–10%. Material screening and iron removal should be considered when recycled pallet or wood waste is used. |
| Production and cycle targets | Define pallet dimensions, mold cavities, shift pattern, operating hours, and target output. A reference automated configuration may be planned around approximately 1,200–1,600 pallets per 24 hours, subject to mold design, press count, cycle time, material handling, and utilization. |
| Adhesive and end-use requirements | Confirm whether pallets are intended for domestic indoor circulation, heavy loads, humid conditions, food or pharmaceutical logistics, or export use. Adhesive type and dosage should be validated through trials; typical starting ranges are approximately 8–10% for MDI and 10–12% for UF or PF, subject to material and performance testing. |
| Facility and utility conditions | Provide separated preparation and forming areas, adequate height and machine-access space, dust control, ventilation, drainage where required, and electrical capacity for motors, heating, hydraulic equipment, and automation. The final layout must be checked against local voltage, frequency, safety, and certification requirements. |
| Automation strategy | Select a full-automatic, semi-automatic, or staged configuration according to budget, labor availability, production volume, and maintenance resources. A semi-automatic concept may retain the mixer and hydraulic press while using purchased prepared fiber and manual material handling; automated conveying, spreading, demolding, and stacking can be added as operating needs develop. |
Modular closed-loop molded pallet production
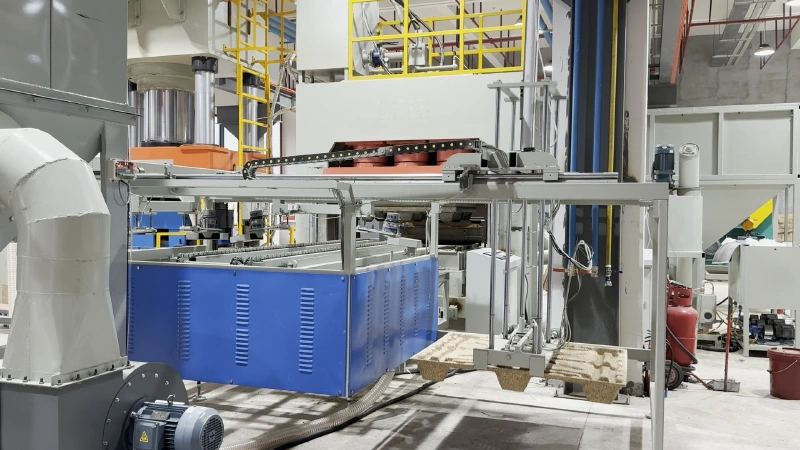
The proposed AutoML system combines material handling and process control into a coordinated production chain. Recycled wood or plant fiber can be screened, crushed, dried, stored in a buffer hopper, and transferred to an adhesive mixing system. A precision gear pump and atomizing spray gun support controlled adhesive application, while a weighing and spreading unit doses and levels the mixed material in the mold. A heated hydraulic press then forms and cures the pallet under controlled temperature, pressure, and hold time. After demolding, a four-axis servo robot can remove and stack finished pallets. Independent loading and unloading equipment allows the forming cell to be serviced or retooled without necessarily stopping every upstream and downstream operation.
Proposed Equipment Configuration
| Component | Proposal-stage scope |
|---|---|
| Material preparation and dust-control system | May include a primary crusher, hammer mill or fine pulverizer, electromagnetic iron separator, conveyors, rotary dryer, airlock, and pulse dust collector. Dryer operation can be configured for electric, gas, biomass, wood waste, fuel oil, or boiler exhaust heat, subject to local engineering and safety requirements. |
| Buffer storage and conveying | A closed buffer hopper with twin screw conveyors and lifting equipment provides dry-material storage between continuous drying and batch adhesive mixing. Conveyors and hopper dimensions are to be selected according to material behavior, throughput, building layout, and anti-bridging requirements. |
| Automatic adhesive mixing system | The mixer can support automatic loading, water and adhesive dosing, and PLC-controlled mixing. A precision gear pump driven by a servo motor supports repeatable adhesive delivery, while an atomizing spray gun is intended to improve fiber coverage and reduce spray blockage. The discharge gate can include air-assisted cleaning to reduce leakage and material buildup. |
| Automatic weighing and spreading machine | Load cells measure the required charge for each pallet, and servo-driven mechanisms transfer the material into the mold. Integrated release-agent spraying and mechanical leveling support repeatable mold filling before the press receives the forming signal. |
| Heated hydraulic molding press and temperature-control unit | The reference press configuration uses a 16,000 kN (approximately 1,600-ton) hydraulic system with controlled closing, pressing, holding, pressure release, demolding, and return sequences. A thermal-oil unit is specified to maintain approximately 150–180°C at the mold, with temperature display, circulation, pressure-relief, cooling, and protective control functions. |
| Robotic demolding and pallet stacking | A four-axis servo robot can use adjustable forks to remove molded pallets from the opened mold and place them in a selected single-station or dual-station stacking pattern. PLC and touchscreen controls can record taught positions, coordinate press signals, and provide operating alerts. |
Engineering coordination for project configuration
EMP can support the next technical review by refining the process flow, equipment scope, mold format, automation level, adhesive approach, facility zoning, utility requirements, and commissioning materials around confirmed project data. The review should include raw-material samples, pallet drawings, required load and environmental performance, target operating schedule, local electrical standards, dust and fire-safety provisions, and the preferred balance between manual and automated handling. Any installation guidance, operator training, service scope, and certification adjustments should be defined separately during the formal technical and commercial review.
Confirm the Inputs Before Final Configuration
Proposal-stage technical solution for project evaluation and configuration review. Final equipment selection, layout, utilities, certifications, operating parameters, and commercial terms require confirmation during technical discussions.
Discuss your molded pallet production requirements with EMP: https://presswoodpallet.com/contact/


