How a Wood Chipping Machine Stabilizes Presswood Pallet Line Throughput
Why the first chipping stage becomes the line bottleneck
In a presswood pallet production line, the first chipping stage determines whether the downstream hammer mill, dryer, glue mixer, and pallet press receive enough material and receive it consistently. EMP Shred matches 45, 55, and 110 kW drum wood chipper models to 4–5, 6–8, and 8–12 t/h requirements, producing controllable 30–35 mm first-stage chips before final milling.
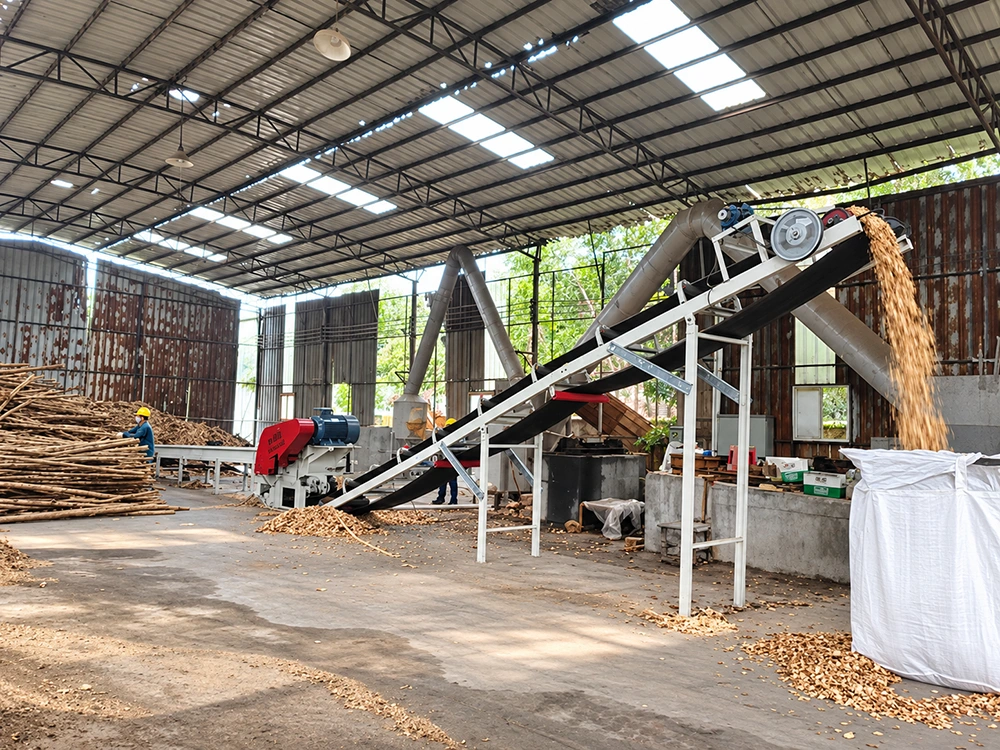
Why outsourced chips or a hammer mill alone are not enough
Buying wood chips can make a pallet plant dependent on an external raw material schedule and price. Manual sawing and splitting also leave an uneven feed for the next process. A hammer mill alone is not a substitute for a wood chipping machine because it is the downstream stage that reduces first stage chips to the final smaller particle range. The practical arrangement is a chipper and hammer mill line, where the drum chipper prepares a consistent feed and the hammer mill completes the reduction.
Match the wood chipper capacity to real wood consumption
EMP Shred provides three electric stationary drum wood chipper ranges: 45 kW at 4–5 t/h, 55 kW at 6–8 t/h, and 110 kW at 8–12 t/h. The 55 kW and 110 kW ranges are relevant starting points for many medium presswood pallet production lines, including projects targeting approximately 3 million pallets per year, but the correct model must be checked against actual wood consumption, operating hours, moisture, density, and the planned hammer mill and dryer capacity. Capacity matching avoids an undersized raw material preparation stage and an unnecessarily large machine.
Knife roller, hydraulic feeding, and the result for downstream milling
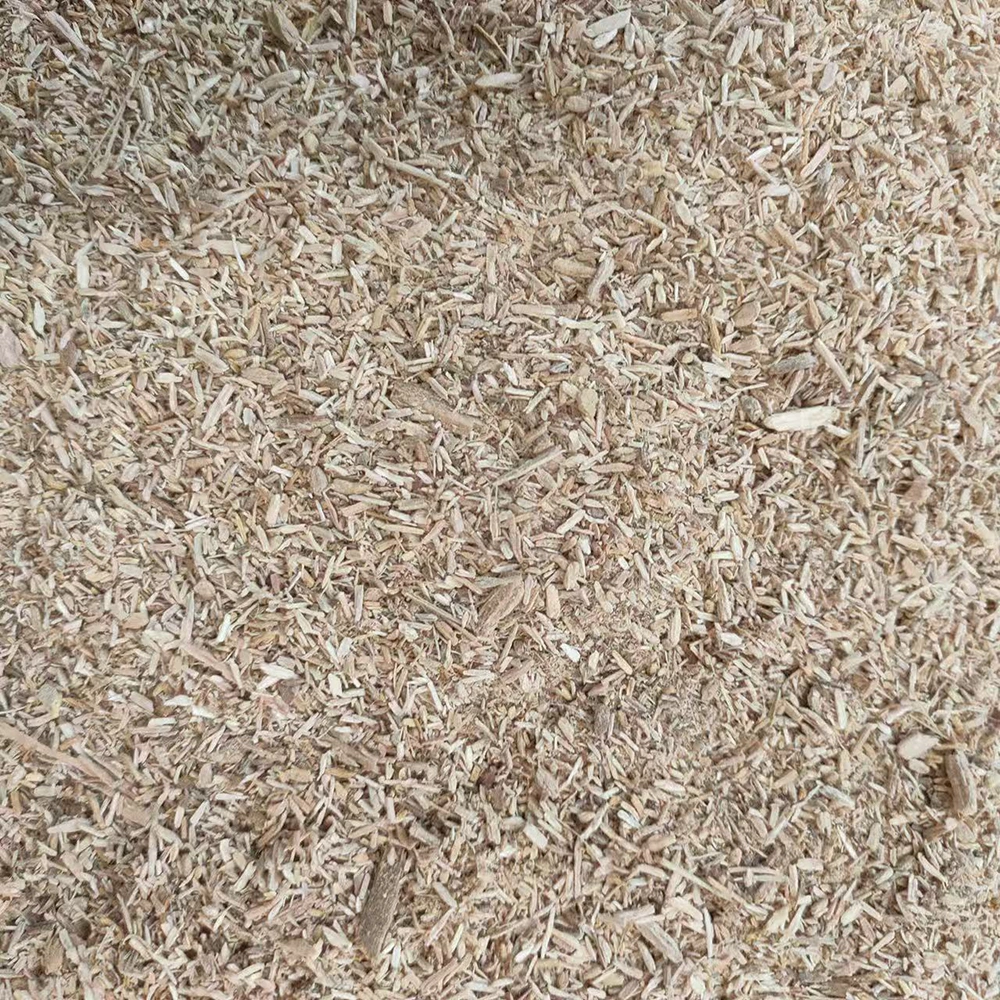
The drum wood chipper uses a knife roller with flying blades and hydraulic feeding to control first stage chip length at approximately 30–35 mm. The factory line image shows chipping, inclined conveying, ducting, and bulk collection; the material image shows the wood chip output transferred to the next process. These chips are not the final molded pallet particle size because the hammer mill still completes reduction to approximately 5–10 mm or the project target. Correctly matched capacity and more uniform chip preparation help maintain feed supply, reduce avoidable downstream grinding load, and support steadier molding results. Ask EMP to calculate capacity from your actual material balance and line schedule.
- body root must include emp-section
- primary CTA must use emp-btn-primary
- CTA href must be /contact/
- publish as post in news category with Shred product metadata


