Same Pallet Spec, Different Batch: Weighing and Dosing Control on a Presswood Pallet Machine Against Manual Batching Rework
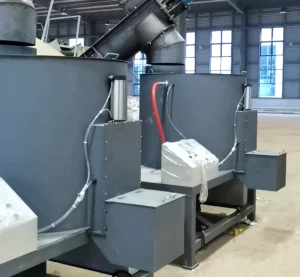
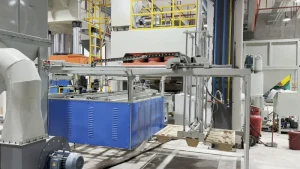
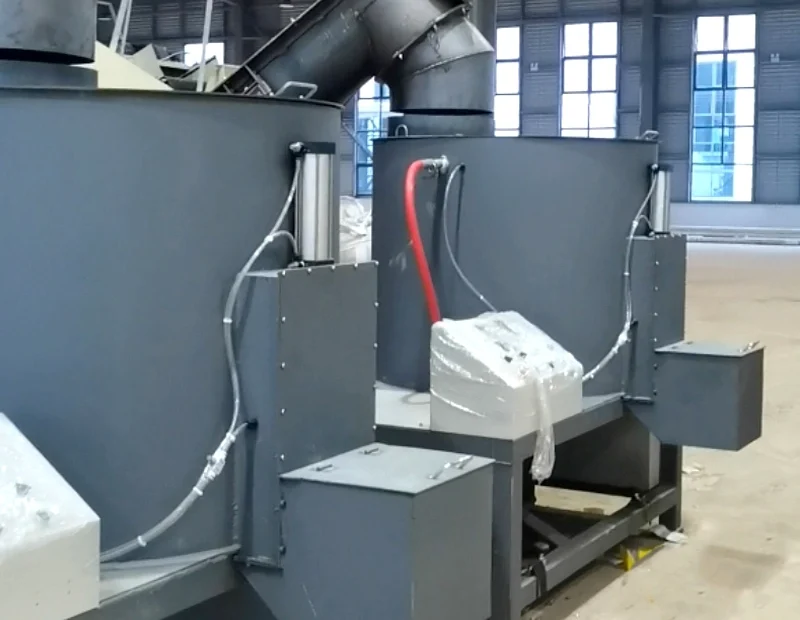
A plant can hold one pallet size, one mold and one recipe and still ship three different batches in three shifts, because on a manual line the fibre load into the cavity and the glue charge in the mixer are still estimates made by a person. This page follows that drift onto an AutoML molded pallet production line, where a rail-mounted weighing and dosing spreader with belt feeders and a metered glue mixer with dosing screw conveyors move those two feeding actions from operator judgement to equipment control, on a 1600T class hot press at 150 to 180 degrees Celsius, 15 to 20 MPa and a 180 to 240 second cycle, with finished density at 0.8 to 1.2 grams per cubic centimetre, MDI commonly around 8 to 10 percent and UF or PF around 10 to 12 percent. The limits are stated plainly: moisture must be matched to the glue system from trial data, tonnage, mold and cycle are confirmed per project in the technical agreement, and the reject and rework improvement has to be measured on the customer’s own fibre and crew rather than assumed.
Repeatable Shift by Shift: How an Automated Pallet Manufacturing Line Takes Presswood Pallet Machine Rhythm Out of Individual Experience
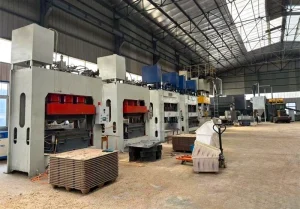
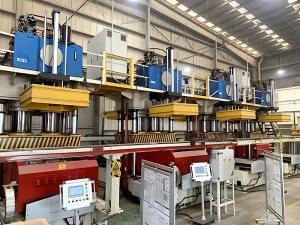
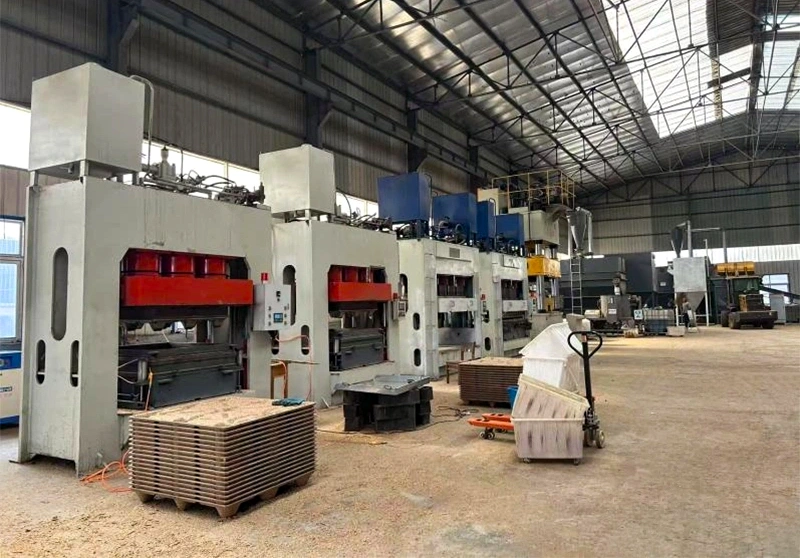
A presswood pallet machine plant loses consistency between people, not inside the press: one shift weighs the fibre by eye, judges moisture by feel, spreads the mat by hand and then waits on the press between the open and close signal, so pallet mass, glue fraction and cycle time all drift with the crew. This page follows that drift onto an automated pallet manufacturing line, where weighing and dosing, glue mixing, spreading, hot pressing, demolding and take-out are sequenced on the line control, with 1200T to 2200T press tiers, a 1600T class reference, hot pressing at 150 to 180 degrees Celsius and 15 to 20 MPa, a 180 to 240 second cycle, MDI at roughly 8 to 10 percent and finished density at 0.8 to 1.2 grams per cubic centimetre. The limits are stated plainly: moisture still has to be matched to the glue system from trial data, tonnage, mold and cycle are confirmed per project in the technical agreement, and automation does not replace training, process confirmation or shop-floor management.
Extra Volume Without Extra Stations: How an Automated Pallet Manufacturing Line Changes Presswood Pallet Plant Expansion
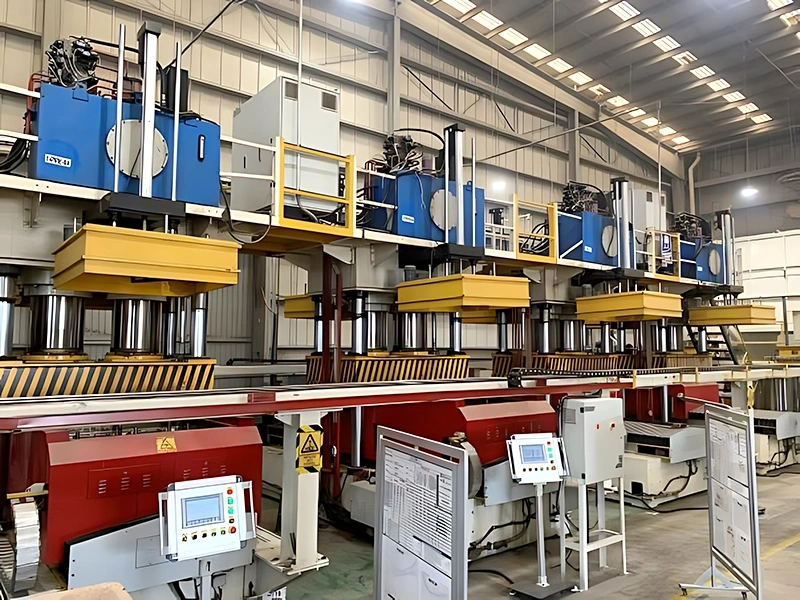
A molded pallet plant that already runs two or three shifts and wants 30 to 40 percent more output usually buys that step as stations: another spreading bay, another take-out hand at every press, another pair at the stack, and a supervisor span that doubles quietly. How a presswood pallet machine line changes the arithmetic: the spreading, dosing, hot pressing, demolding and conveyor stacking handovers that the automated pallet manufacturing line owns, the 1200T to 2200T press tiers and the 180 to 240 second cycle that set real capacity, the semi-automatic versus fully automatic boundary, and the four checks (press count, cycle time, shift pattern, site conditions) a plant should verify before treating volume growth as a configuration question rather than a headcount one.
Presswood Pallet Machine Take-Out Stage: Four-Axis Servo Stacking That Ends Repeated Manual Pallet Handling at the Press Exit
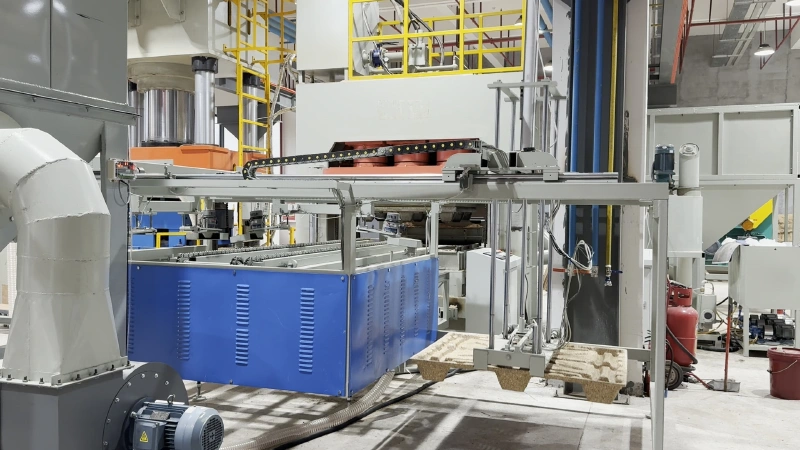
Every hot press cycle on a molded pallet production line ends with an open die and a cured pallet that has to be taken out and stacked, and on many presswood pallet machine lines that last step is still manual: the pace drifts with the shift, the press waits between the open and close signal, and an operator works beside tooling held at 150 to 180 degrees Celsius. AutoML configures a four-axis servo robot at the back end of the line to follow the process motion, take the pressed pallet out and place the stack, so the repeated handling after pressing is carried by the machine. Press references, tonnage tiers, demolding and conveyor evidence are set out plainly, and robot motion, safety zone and stacking pattern are stated as project confirmations rather than fixed promises.
Steady Packaging Customers, No Pallet Line: Turning Outsourced Pallet Demand Into In-House Output With a Presswood Pallet Machine
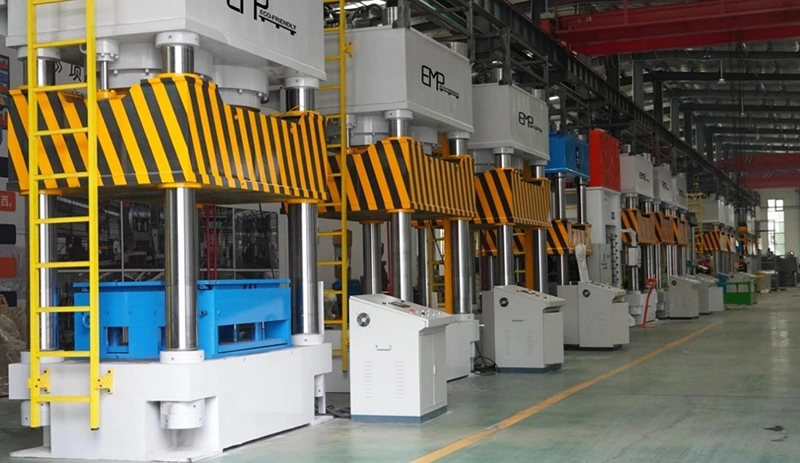
A packaging distributor can hold the accounts, the call-off schedule and the whole consumables basket and still resell pallets it does not control. How a presswood pallet machine moves that volume in-house: the molded pallet production line from crushing and drying through glue mixing and hot pressing, semi-automatic versus fully automatic costing, the 1200T to 2200T tonnage tiers and the pressing window, and the four conditions (real pallet demand, a channel for a molded unit, utilities and layout, an investment case) a supplier should verify before quoting a pallet contract.
From Steady Pallet Volume to In-House Output: Which Plants Should Stop Buying and Run a Presswood Pallet Machine
A steady pallet count still reprices whenever sawn lumber, freight and treatment chamber hours move, so the real question is not machine price but whether in-house molded output beats continued purchase on your own numbers. Which plants fit that test, what a nailed wood pallet purchase price leaves out, where the AutoML molded pallet production line sits in the cost chain, and the four conditions (fibre, utilities, shift labour, order discipline) that decide make versus buy, with the parameters, investment references and limits stated plainly.
Lightweight Packing Spec Change: Turning a New Customer Size Into In-House Output With a Presswood Pallet Machine
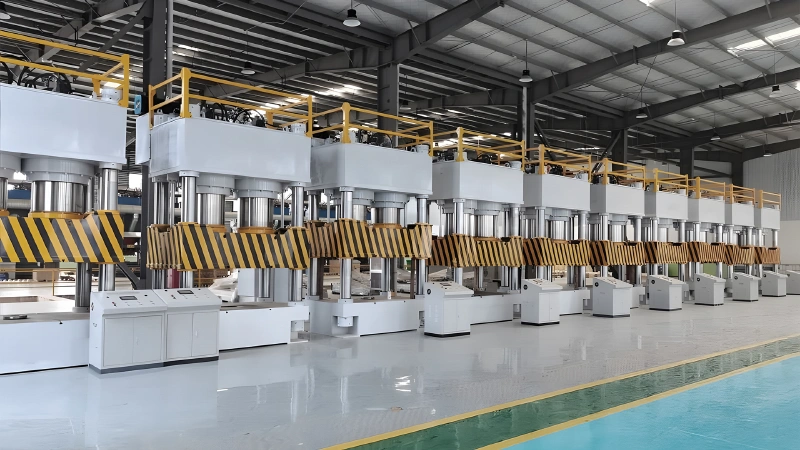
When a customer lightens the pack, the pallet spec arrives with a new size, a new load class and a new volume, and a bought-in program or a nailing cell may not answer it. How a presswood pallet machine turns that changed order into in-house molded output, which tonnage tiers, pressing window and mold questions to test, and the drawing, duty cycle and order volume to send first.
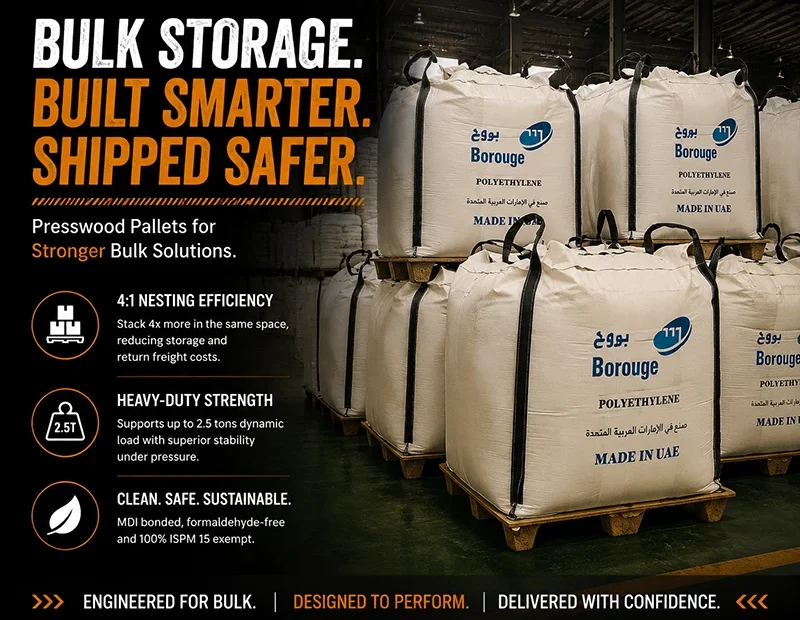
Bulk Chemical Raw Material Warehouse: Nesting a Presswood Pallet Pool Into a Quarter of the Empty Bay Floor
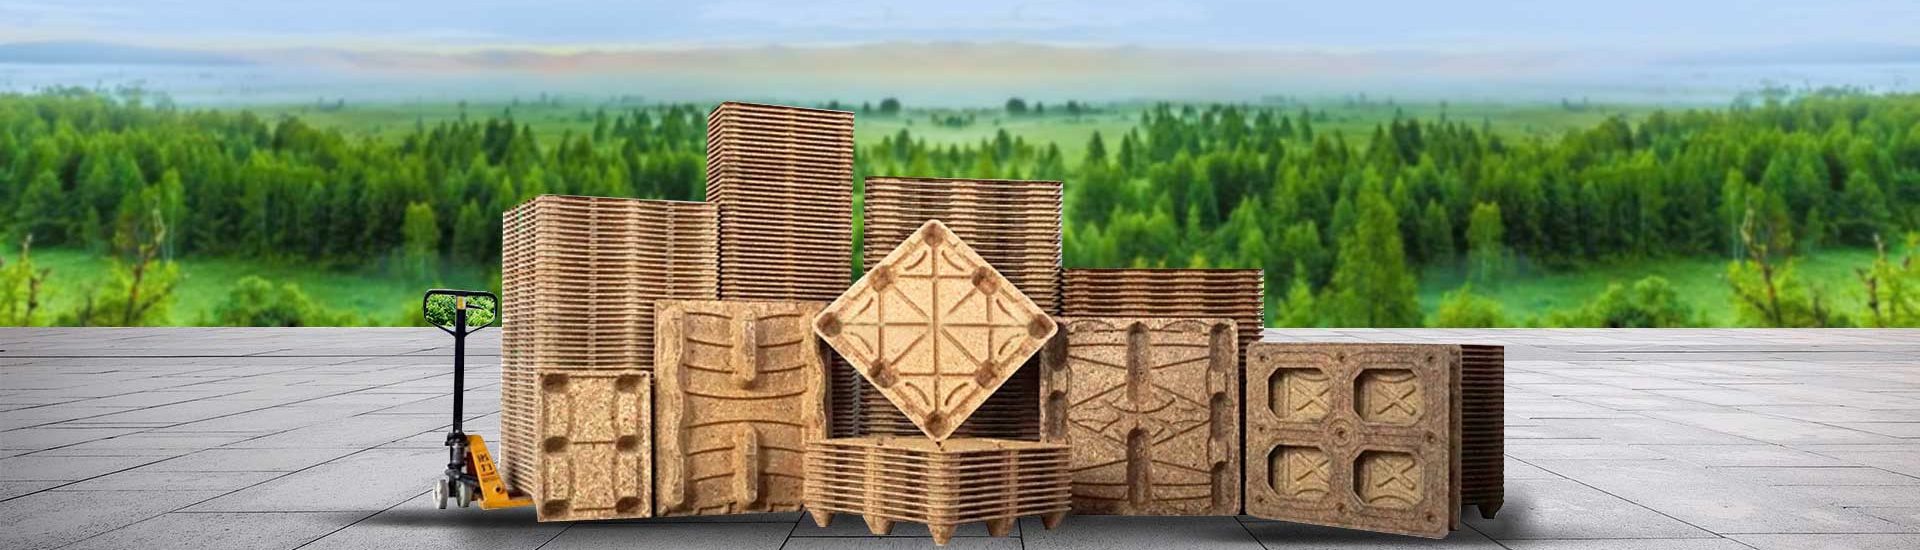
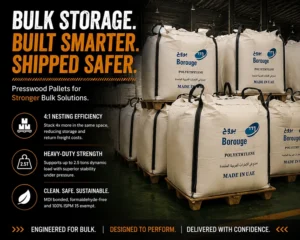
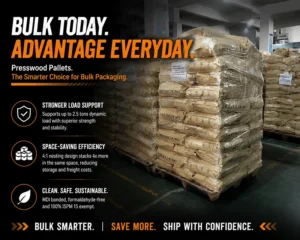
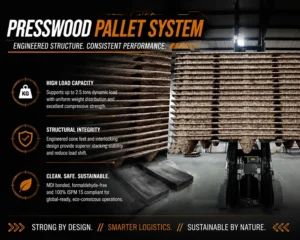
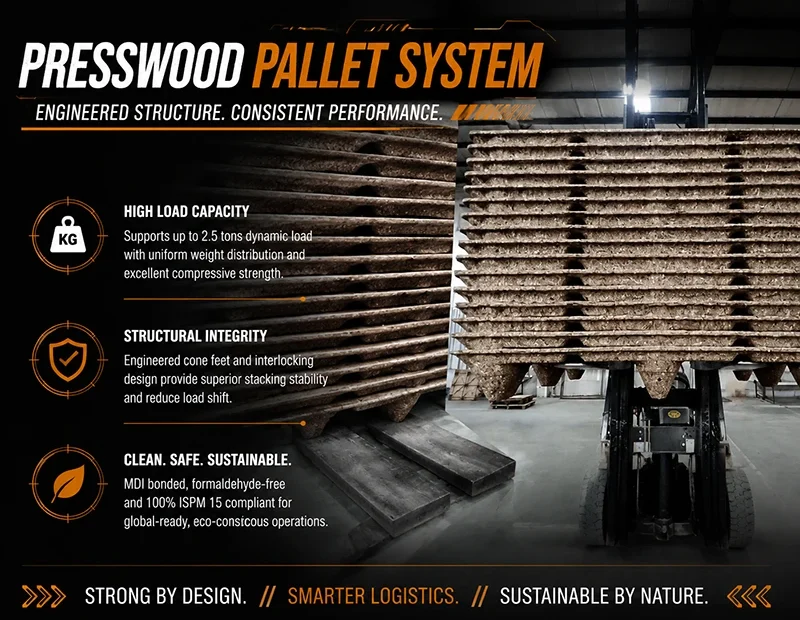
A bulk chemical raw material store runs out of floor on the empty pool, not on the load: bagged filler, resin sacks, drummed intermediates and one-way export lots all pull pallets through the same bay, and a rigid solid wood or heavy duty plastic pallet claims the full deck footprint whether it carries two tonnes or nothing, because its fixed feet land on the unit below instead of settling into it, so the same count stacks to about 2.7 metres instead of 0.75 metres. Ampallet is a nestable presswood pallet molded in one piece from recovered wood fibre and an MDI binder on a 1600 ton press at about 150 to 180 degrees Celsius, with inverted cone feet that settle into the deck recesses below at about a 4 to 1 nesting ratio, guide slots and four-way entry: 1200 x 800 x 125 mm nine-leg at about 13 to 14 kg with 2000 kg dynamic and 6000 kg static load, 1140 x 1140 x 135 mm drum unit at about 17 kg with 2500 kg dynamic and 7000 kg static, 800 x 600 x 125 mm six-leg at about 6 kg. Published positioning places empty pallet stacking saving near 70 percent with storage capacity at about 2.5 times on the same floor. Limits are stated plainly: floor saving and nesting are recalculated per site and per mold, the nestable single-face unit is not a long-term racking pallet, load is confirmed per specification, and a fumigation-free reading stays a destination rule and forwarder question.
Batch Consistency Instead of Batch Lottery: A Presswood Pallet Held to ±2 mm for a 24/7 Unmanned Warehouse Cell
A chemical or material supplier that runs internal moves on AGVs, an automated store and a palletizing robot finds the pallet is the last part of the cell still arriving with millimetres of variation: a nailed heat treated wood pallet can spread 10 to 15 mm in length between units of a single delivery, so a fork misses the pocket, a photo-eye reads a deck edge that is not there and the line faults into a manual re-stack. Ampallet is a molded wood pallet pressed in one piece from recovered wood fibre and an MDI binder on a 1600 ton press at about 150 to 180 degrees Celsius to about 9 percent finished moisture, with deck, reinforcing ribs and nine conical feet out of one steel mold, so outside length, fork pocket and deck plane are set by the tool: height at plus or minus 2 mm, corner height difference at 3 mm or less, round corners at R25 or R35 within 2 mm, fork entry at 92 or 96 plus or minus 3 mm, four-way entry and molded guide slots. Model references: 1200 x 800 x 125 mm nine-leg at about 13 to 14 kg with 2000 kg dynamic and 6000 kg static load; 1140 x 1140 x 135 mm drum unit at about 17 kg with 2500 kg dynamic and 7000 kg static; 800 x 600 x 125 mm six-leg at about 6 kg with 1000 kg dynamic and 3500 kg static. Limits are stated plainly: plus or minus 2 mm is a tooling and inspection position on the confirmed footprint rather than a promise for every custom mold, the AGV fork, roller, pin stop and sensor interface are confirmed per lane with the integrator, the nestable single face unit is not a long term racking pallet, load is confirmed per specification, and a fumigation free reading stays a destination rule and forwarder question.
Nail-Free Pressed Wood Pallet: Ending FIBC Puncture, Drum Coating Scuff and Hand Injury From One Deck Surface
A chemical, mineral or food ingredient site that loads FIBC jumbo bags and coated steel drums keeps the pallet in direct contact with the product, and on a nailed solid wood pallet that contact face carries steel fastener heads and lifted splinters. Ampallet is a presswood pallet molded in one piece from wood fibre and an MDI binder, with no nail, no screw and no separate foot, so bag weave is not abraded, drum coating is not scraped to bare steel and the operator is not reaching past a fastener. Model references: R1414 at 1140 x 1140 x 135 mm, nine legs, about 17 kg, 2500 kg dynamic and 7000 kg static load, 96 mm fork entry; R1208 at 1200 x 800 x 125 mm, 13 to 14 kg, 2000 kg dynamic and 6000 kg static; R0806 at 800 x 600 x 125 mm, six legs, about 6 kg, 1000 kg dynamic and 3500 kg static, with four-way entry, guide slots and nesting near 4 to 1. Limits are stated plainly: a one-piece body is replaced rather than re-boarded, the nestable single-face unit is not a long-term racking pallet, load follows the confirmed specification, and a fumigation-free reading stays a destination rule and forwarder question.