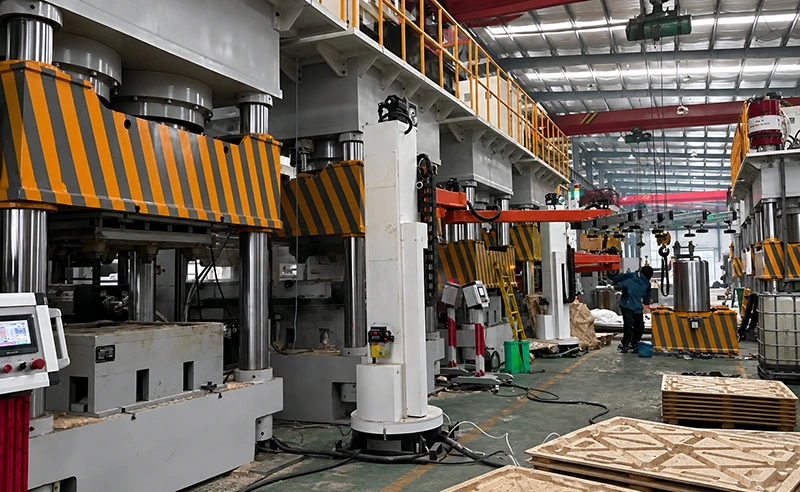
AutoG Automatic Pallet Take-Out Robot: Breaking the Press-Exit Takt Bottleneck That Tonnage Alone Cannot Fix on a Presswood Pallet Line

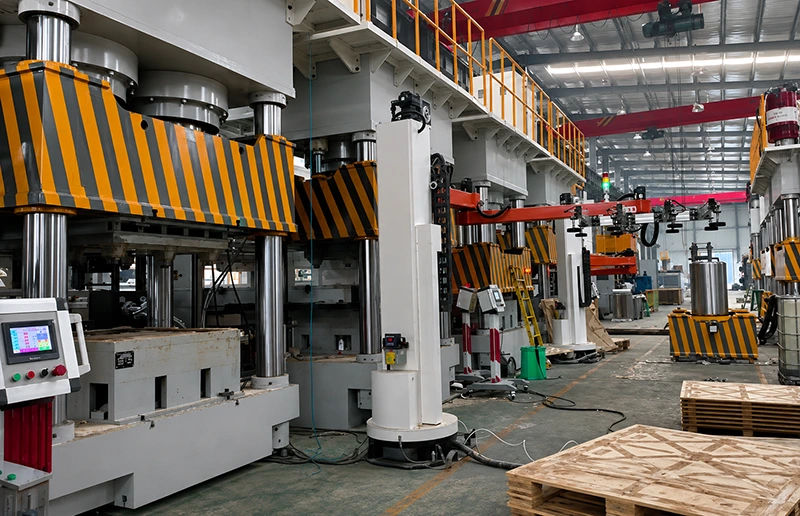
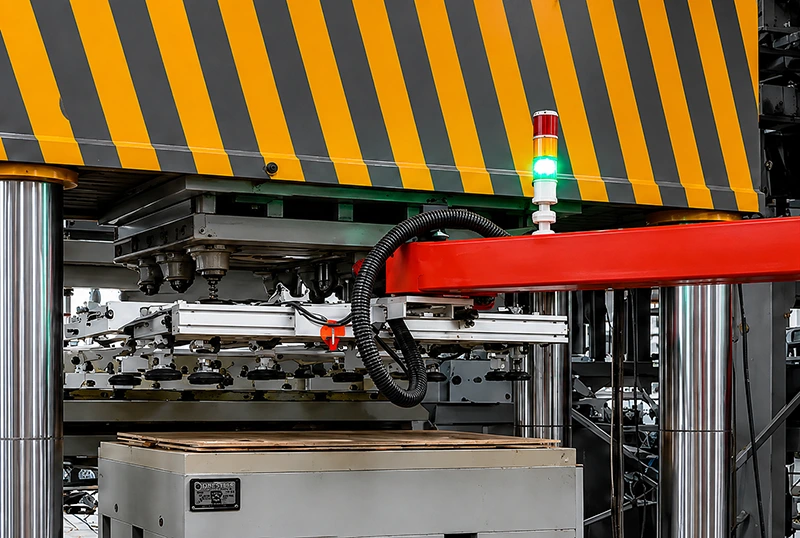
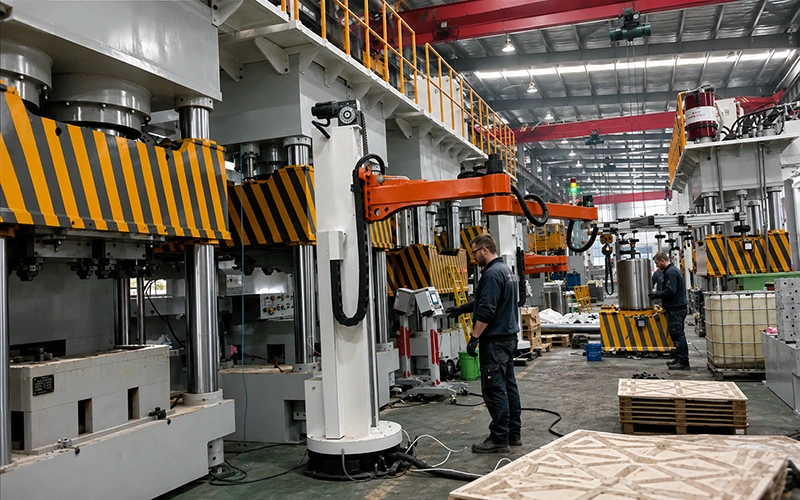
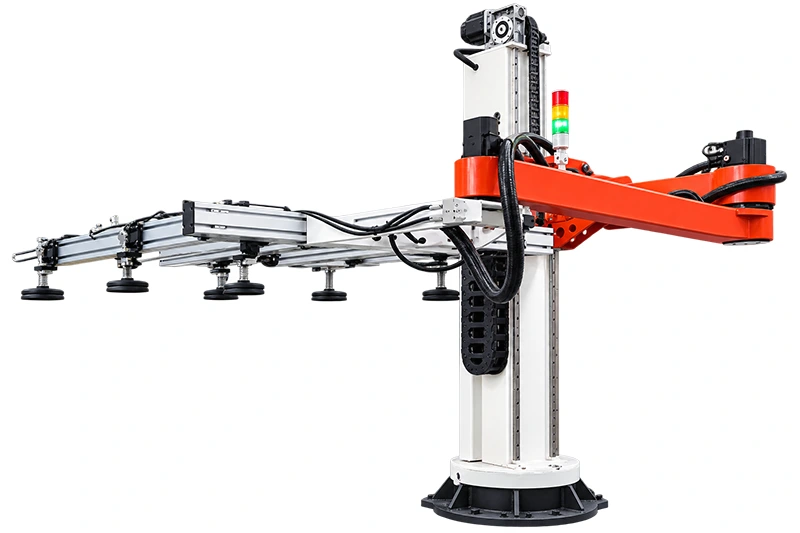
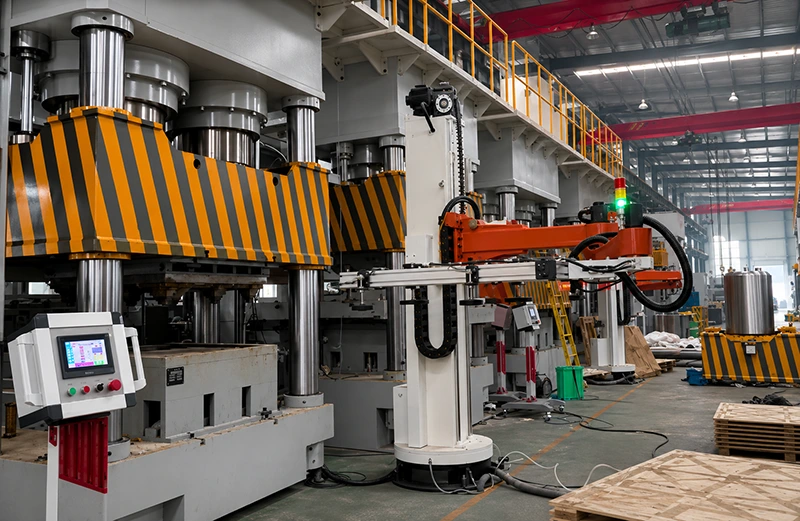
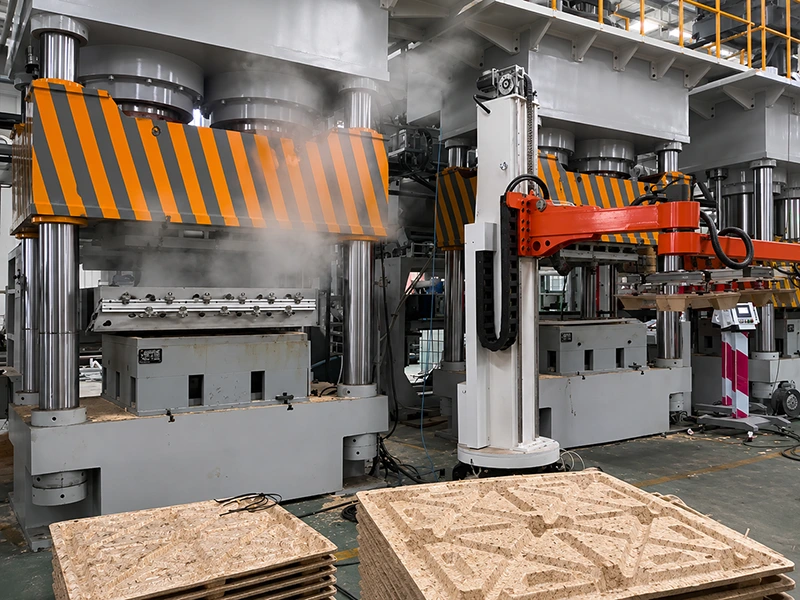
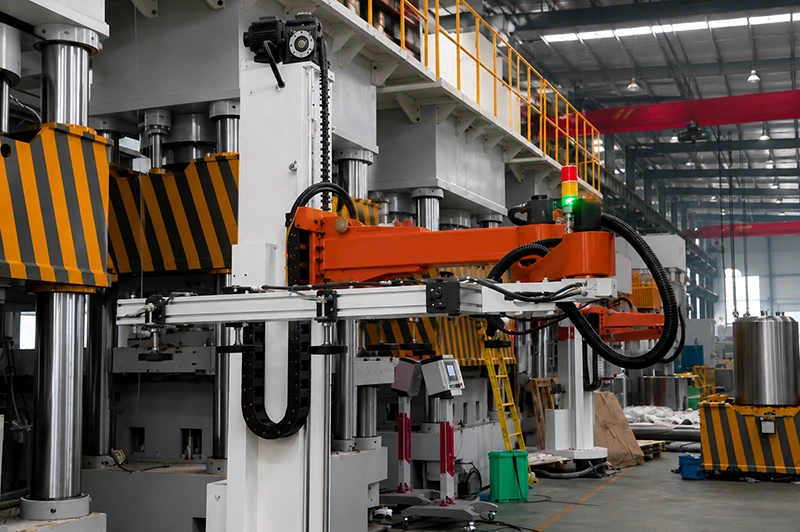
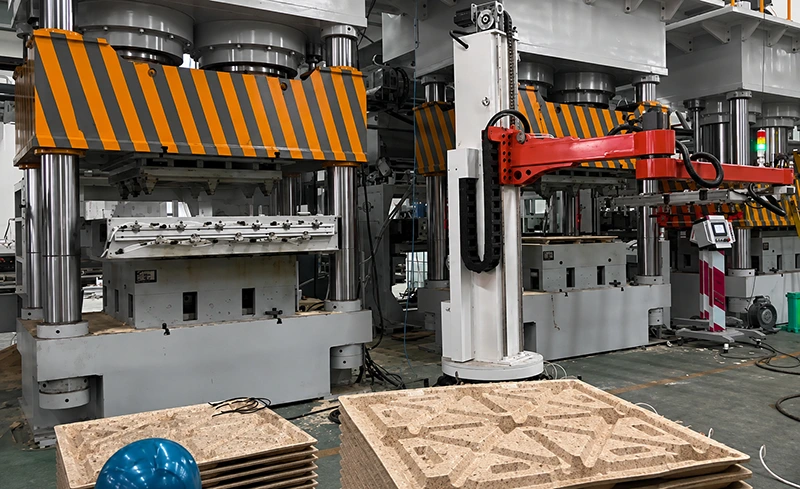
A presswood pallet plant buys tonnage and still loses output at the die exit: a manual take-out post cannot be timed to the press open and close signals, so a 1250 to 1600 ton press waits on a person every cycle, line OEE drops and unit cost carries the delay plus one operator per press on every shift. AutoG is the automatic pallet take-out robot from EMP, delivered as the press exit take-out and automatic stacking cell on a presswood pallet production line: the take-out motion is coordinated with the press open and close signals on the line PLC, a vacuum suction cup end effector takes the freshly pressed pallet at about 80 degrees Celsius without a cooling wait, transfers it by vacuum suction and stacks it where it leaves the gripper, and one arm alternately tends two presses as a dual press tending cell, so press exit manning is set per press pair instead of per press. Limits are stated plainly: rated load, working radius, repeat accuracy, suction and vacuum configuration, footprint, power and air demand, control interface detail and robot body source stay project confirmed; the 1250 to 1600 ton range, the four to five minute MDI cycle, continuous running and the replacement of about two take-out operators are supplier statements; the 80 degrees Celsius figure is quoted from the EMP equipment centre description; no ROI, payback or hourly output is claimed; and the unit is the press exit take-out and stacking device on a presswood pallet line, not the press itself, not the crush, dry or glue stage and not an independently running line.